Introduction: Overcoming Site Infrastructure Bottlenecks in Eastern India
For project managers, lead engineers, and B2B procurement teams spearheading industrial development across Eastern India, establishing a reliable and immediate on-site administrative base is a non-negotiable priority. The region is experiencing massive infrastructure growth, from heavy manufacturing expansions along the NH6 Corridor to large-scale port developments in Haldia. However, waiting months for traditional brick-and-mortar facilities to be constructed can severely derail your project timelines, inflate initial capital expenditures, and stall engineering operations before ground is even fully broken. The most strategic, agile, and cost-effective solution is to invest in a prefabricated portable cabin for office operations.
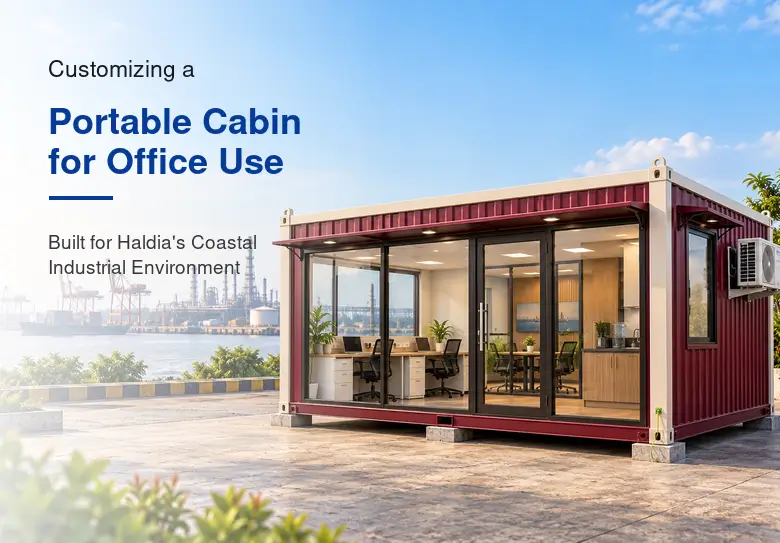
This highly adaptable, heavy-duty workspace entirely bypasses the unpredictable delays of civil construction. By utilizing a modular approach, your remote administrative teams, site engineers, and project executives can plug in and begin working immediately on day one in a fully climate-controlled, secure environment. Selecting the correct sizing, dimensions, and structural specifications for your Modular Office Cabin is crucial to maintaining daily workflow efficiency, ensuring employee comfort, and optimizing your site’s physical footprint. This comprehensive guide will walk you through the precise specifications, layouts, and materials required to deploy the ultimate remote command center for your next major project.
Core Guidelines: Sizing and Layout Planning for Optimal Workflow
Choosing the correct dimensions for your portable cabin for office use is not merely about fitting desks into a box; it is about engineering a workspace that reflects your team’s operational hierarchy and daily workflow. Standard footprints are designed to maximize every available square foot while maintaining a comfortable, standard internal clear height of 8.5 feet to prevent the space from feeling cramped during long working hours.
When planning your site infrastructure, B2B procurement teams must evaluate their immediate headcount alongside potential project scaling. Below are the standard dimension guidelines and layout strategies utilized by top project managers across the NH6 Corridor and beyond:
- Compact QA/QC and Security Cabins (10 ft x 10 ft or 15 ft x 10 ft): These smaller units are engineered with a heavy-duty 60×60 mm base SHS (Square Hollow Section) frame and 72×72 mm corner posts. They are the perfect size for localized gate check-posts, material testing laboratories, or single-supervisor workstations where site space is at an absolute premium. They offer enough room for a single desk, filing cabinets, and essential IT infrastructure.
- Standard Project Engineer Cabins (20 ft x 10 ft): This represents the industry-standard size for mid-level administrative needs on active construction and industrial sites. A 200-square-foot footprint comfortably accommodates dual-desk managerial setups or open-plan administrative team stations. This dimension allows for ample circulation space, essential blueprint review tables, and dedicated corners for communications and server equipment.
- Large Command Centers and Boardrooms (30 ft x 10 ft or 40 ft x 10 ft): Upgraded with a reinforced 72×72 mm base SHS and massive 90×90 mm corner posts to handle the extended load, these expansive units are perfectly suited for primary project headquarters. A 40-foot cabin provides massive internal volume that can be partitioned into multi-workstation setups, enclosed private managerial suites, and large contractor consortium meeting rooms.
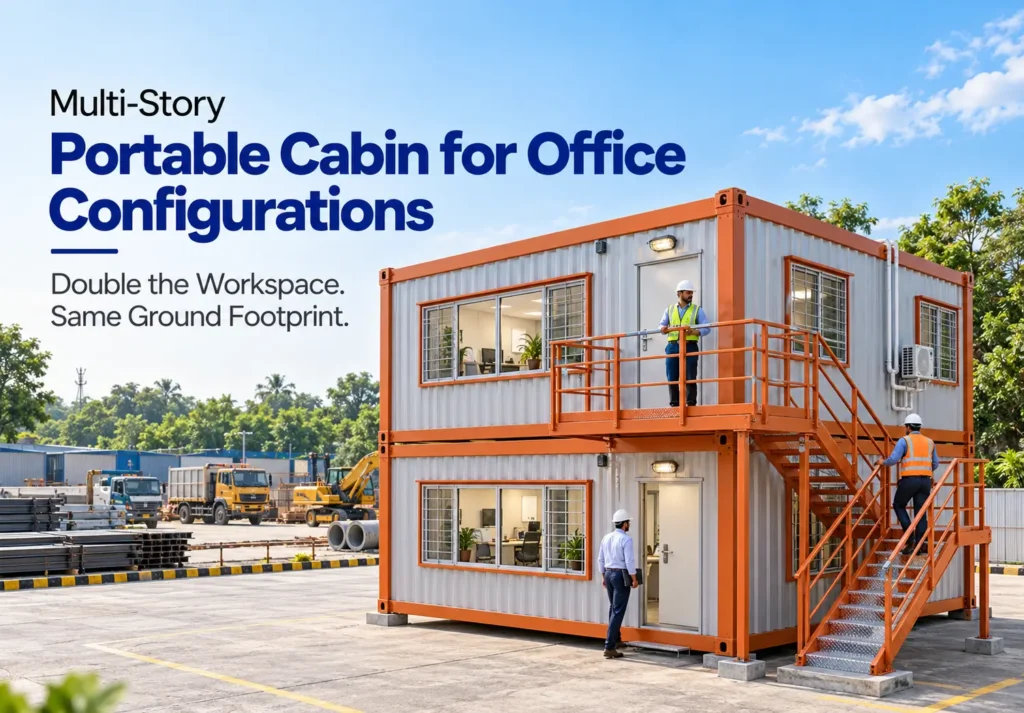
- Multi-Story Configurations (G+1/G+2): When horizontal ground space is restricted, these heavy-duty structures are engineered to be stackable. By utilizing external metal staircases and reinforced roof frames, you can double your administrative square footage without expanding your site footprint.
Key Features & Materials: Uncompromising Durability and Customization
A true heavy-duty Modular Office Cabin must be capable of withstanding punishing coastal monsoons, extreme summer heat, and frequent crane relocations across rough terrain. The engineering that goes into a premium portable cabin separates a temporary shed from a long-term, reusable corporate asset.
Structural Integrity and Mild Steel (MS) Defense
The structural shell of a high-grade modular cabin relies on fully continuous-welded 1.2 mm thick corrugated Mild Steel (M.S.) exterior sheets. This ensures an uncompromising, weather-tight monolithic box. To combat the high humidity and corrosive environments often found in Eastern India, every inch of the steel frame undergoes a rigorous anti-rust treatment featuring industrial Red Oxide primer, followed by two thick coats of premium weather-grade Synthetic Enamel paint.
Advanced Thermal and Acoustic Insulation
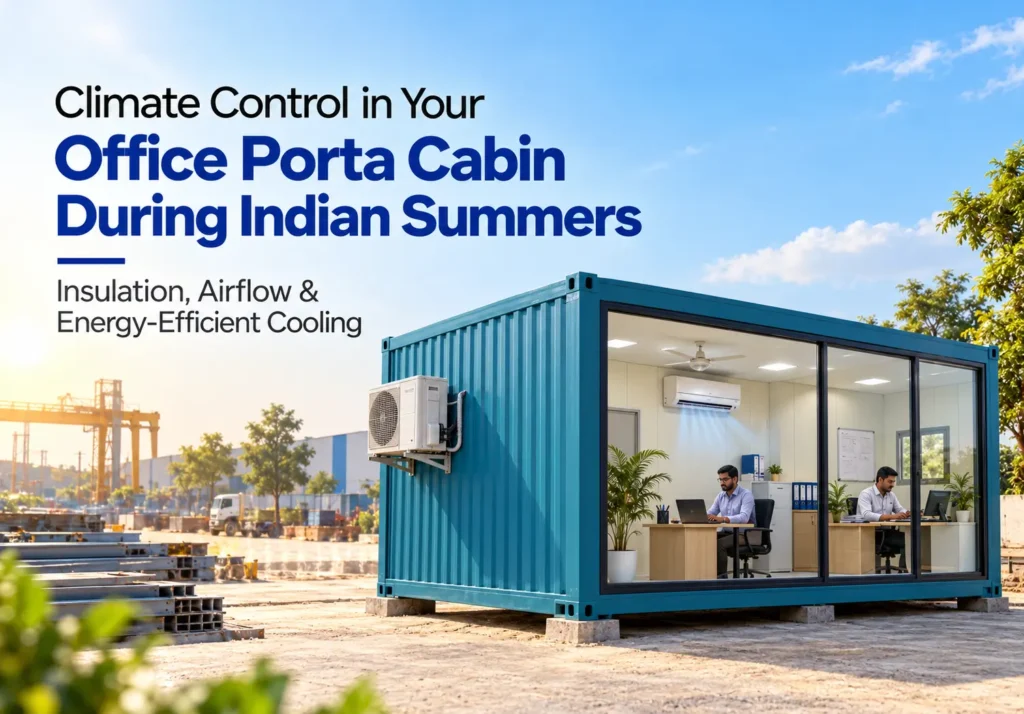
An uninsulated steel structure is uninhabitable in extreme climates. To ensure maximum climate-controlled comfort, premium cabins are lined with a 25 mm thick Glasswool or high-density Polyurethane Foam (PUF) insulation core. This robust thermal barrier keeps the interior cool in the summer and retains warmth in the winter, drastically reducing air conditioning power consumption. Furthermore, this insulation, combined with 9 mm Particle Board or 4 mm Aluminium Composite Panel (ACP) wall cladding, acts as a powerful acoustic dampener against deafening heavy machinery noise.
Industrial-Grade Flooring Systems
Heavy boots and constant foot traffic require flooring that will not warp or degrade. The foundation consists of an 18 mm heavy-duty Cement Fiber Board or marine-grade plywood base. This is topped with a 1.5 mm thick, wear-resistant, and anti-skid PVC Vinyl mat. For executive cabins, vitrified tiles can be installed to elevate the corporate aesthetic.
Turnkey Electrification and Plug-and-Play Readiness
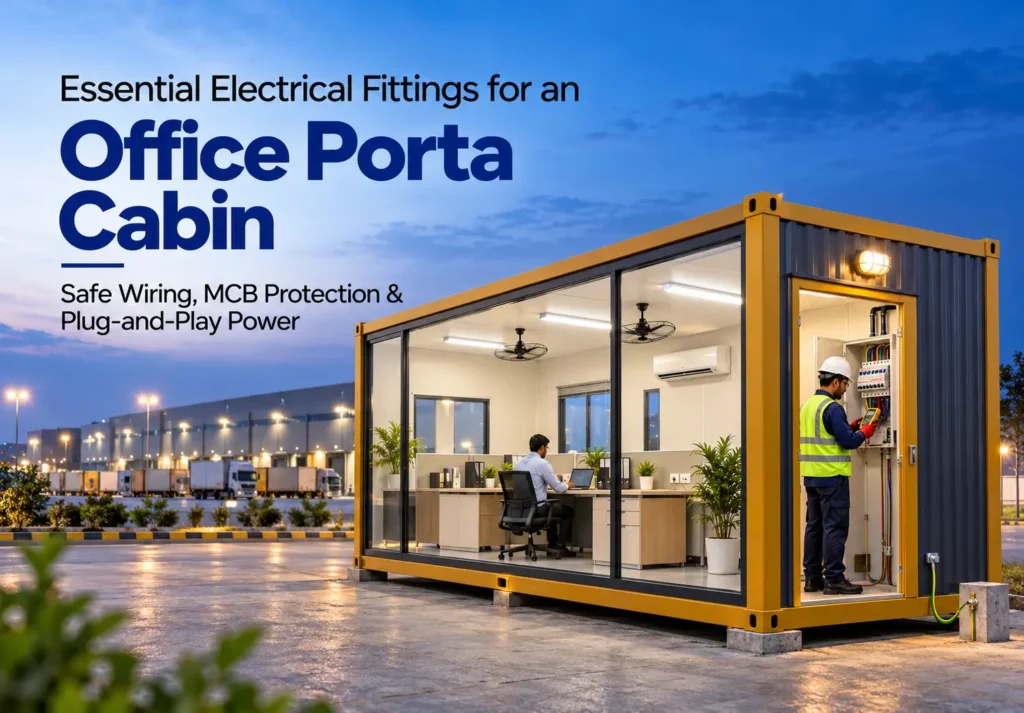
Every unit arrives at your site fully equipped with factory-tested concealed wiring using ISI-certified fire-retardant copper cables. The electrical layout includes dedicated high-load MCB distribution boards, strategic AC provisions, flush-mounted LED panel lights, high-speed ceiling cage fans, and external bulkhead lighting. Simply connect the exterior input socket to your site’s main power grid, and your remote team is instantly operational.
Comparisons: Modular Solutions vs. Traditional Civil Construction
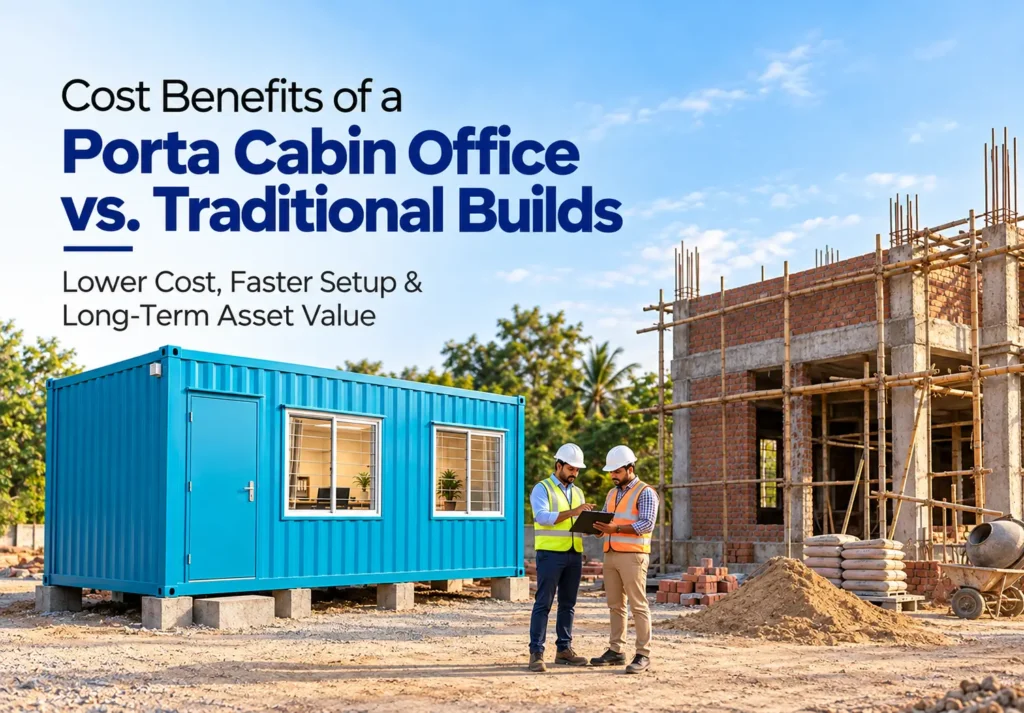
When B2B procurement teams evaluate site infrastructure investments, the comparison between a portable cabin for office use and traditional civil construction heavily favors the modern modular approach. The financial and operational benefits of modular infrastructure are transforming how remote sites are managed.
- Zero Site Downtime and Rapid Deployment: Traditional brick-and-mortar buildings require municipal permits, deep foundation digging, prolonged material curing times, and highly unpredictable local labor schedules. A modular unit is manufactured off-site in a controlled factory environment and delivered ready for immediate deployment. You bypass months of delays and launch your site operations in a matter of days.
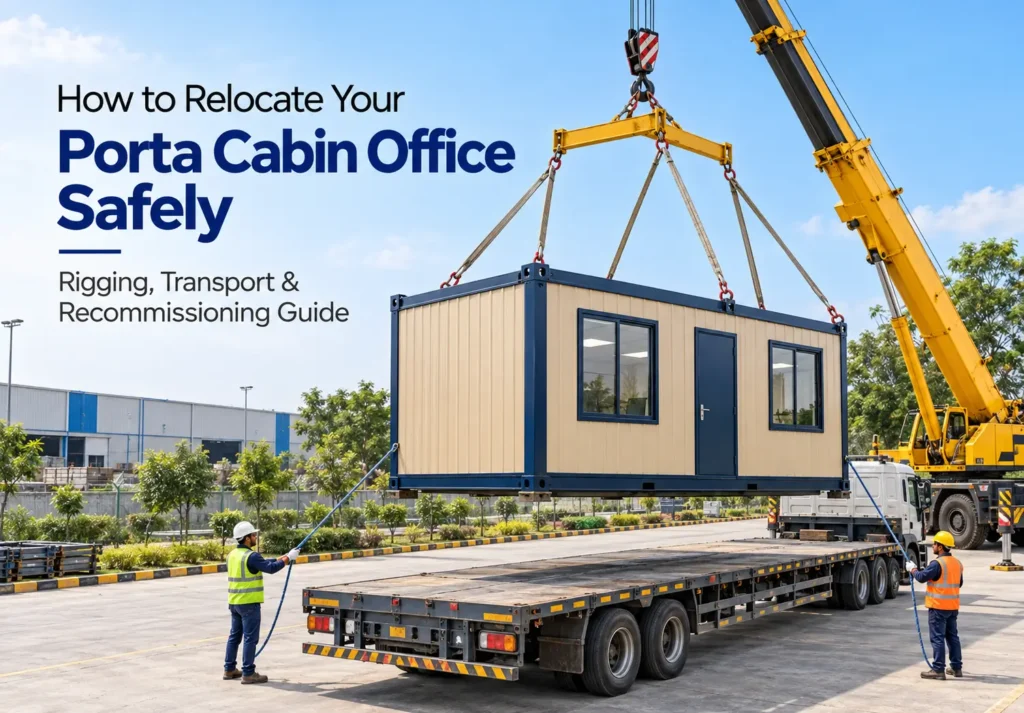
- Capital Preservation and Unmatched Mobility: A concrete building must be demolished at the end of a project, resulting in a total loss of structural capital and generating massive amounts of environmental waste. Conversely, a modular cabin features integrated top rigging posts and heavy corner castings, allowing it to be hoisted by a standard crane onto a flatbed trailer and transported directly to your next site without any structural degradation. You buy the asset once and reuse it for decades.
- Predictable Budgeting and Fixed Costs: Civil construction is plagued by hidden costs, weather-delayed labor charges, and wildly fluctuating raw material prices. Modular manufacturing provides procurement teams with a fixed, transparent, upfront price point with zero hidden fees, making budget approvals seamless and highly predictable.
- Eco-Friendly Footprint: Civil builds heavily disrupt local topsoil and generate non-recyclable debris. Prefabricated cabins are dropped onto simple leveled blocks or concrete pads, leaving a near-zero environmental footprint when the project concludes.
Frequently Asked Questions (FAQ)
What are the standard dimensions for a Modular Office Cabin?
Standard manufactured footprints are highly versatile to meet various site demands. They typically include 10 ft x 10 ft, 15 ft x 10 ft, 20 ft x 10 ft, 30 ft x 10 ft, and 40 ft x 10 ft, all constructed with a comfortable internal clear height of 8.5 ft to ensure a spacious and ergonomic working environment. Custom lengths, multi-module configurations, and split internal partitions can also be easily fabricated based on specific B2B site requirements.
How long will a steel portable cabin for office use last?
When engineered by a certified manufacturer, these heavy-duty structures are built to last. Thanks to the heavy-gauge SHS framing, continuous welding, industrial Red Oxide anti-corrosive primers, and weather-grade enamel paints, a premium modular cabin boasts a structural lifespan of 15 to 20+ years under regular maintenance, even in demanding high-humidity industrial zones.
Can these cabins be easily relocated along the NH6 Corridor?
Absolutely. The entire structure is specifically engineered as a rigid, monolithic steel box designed for constant mobility. The integrated heavy-duty corner posts and top lifting lugs allow for a direct, safe crane hoist onto transport trailers. This means the unit can be moved instantly across bustling industrial belts like the NH6 Corridor, Dankuni, or Haldia without requiring any dismantling or risking structural compromise.
Are the internal electrical systems safe for heavy IT and AC loads?
Yes. The electrical infrastructure is designed for modern corporate demands. All wiring is entirely concealed using fire-retardant cables. The cabins feature dedicated high-load MCB (Miniature Circuit Breaker) wiring, standard 6A/16A switch sockets for servers and workstations, and dedicated heavy-duty lines for air conditioning units to ensure absolute safety and prevent overloading.
Why Choose PortaSpaze for Your Modular Infrastructure
Do not let slow civil construction dictate your project timelines or drain your capital expenditure. As a premier manufacturer in Eastern India, PortaSpaze goes far beyond basic steel fabrication. We engineer rugged, heavily insulated, and highly professional workspaces tailored to your exact operational dimensions, workflow requirements, and corporate aesthetics.
Whether you require a compact quality-control security booth, a sprawling 40-foot multi-desk command center, or a multi-story administrative complex, our team delivers turnkey reliability that survives the harshest environments. Upgrade your site infrastructure today and ensure your engineering team has the perfect Modular Office Cabin to drive project success from day one. Contact PortaSpaze to speak directly with a project engineer and request a comprehensive custom quote for your next heavy-duty deployment.